Polymer Dosing for Dewatering: Getting Cake Solids Right
Underdosing and overdosing polymer both look similar on the belt press until you know what to check.
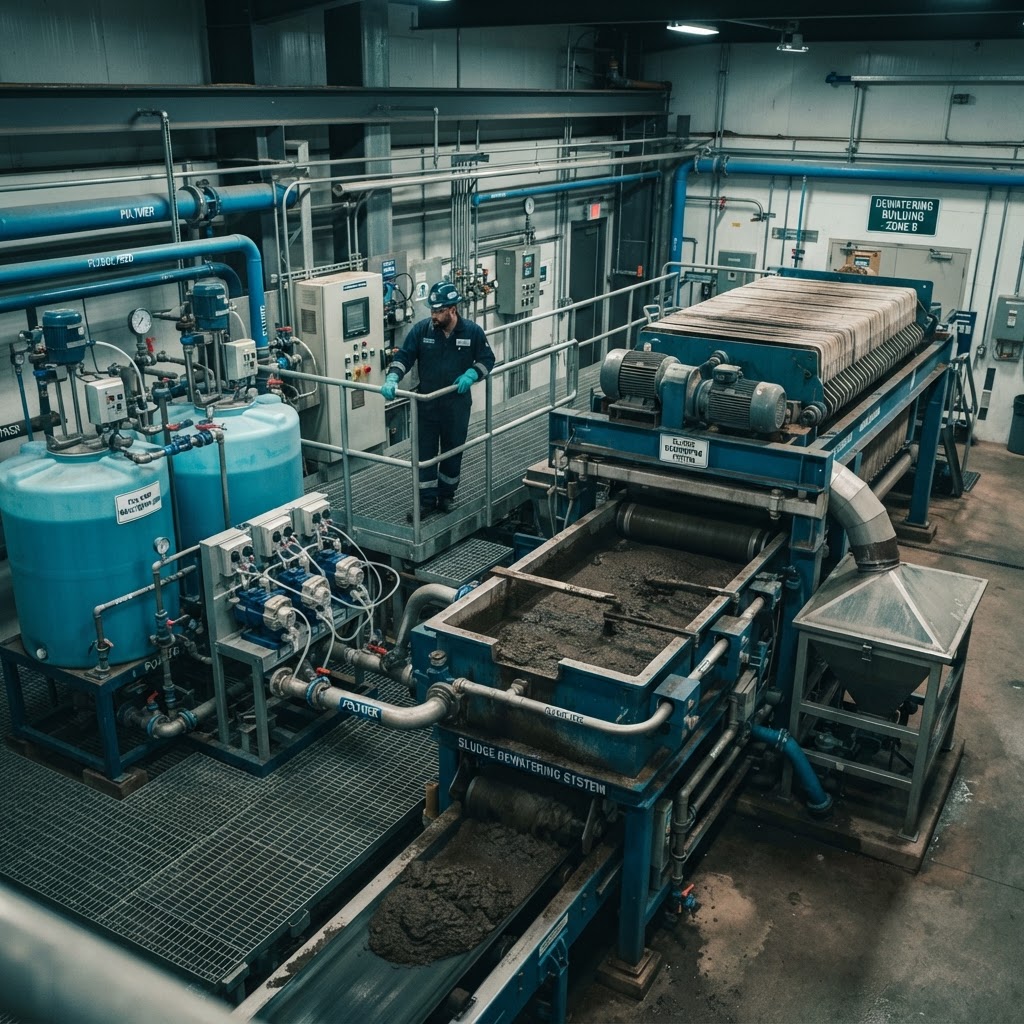
Polymer conditions sludge by neutralizing surface charges on the particles, allowing them to clump into larger flocs that release water more easily under mechanical pressure. Get the dose wrong in either direction and you'll see the same symptom on the belt: poor cake solids and cloudy filtrate, which is why so many operators chase the wrong fix.
Underdosing shows up as a wet, sloppy cake and filtrate that's visibly turbid with fines that never flocculated. The instinct is often to increase belt tension or slow the feed rate, but if the floc structure was never formed properly, mechanical adjustments downstream can't compensate. Increase dose in small increments, typically 2–5 lbs of active polymer per dry ton as a starting adjustment, and watch filtrate clarity before making a second change.
Overdosing is easy to miss because cake solids can look acceptable at first glance, but you'll typically see excess polymer in the filtrate (a slick or foamy appearance) and, over time, rising polymer costs without a proportional cake solids improvement. Past a certain point, added polymer doesn't improve dewatering further, it's simply wasted, and in some cases it can actually re-disperse floc that formed correctly at a lower dose.
Feed sludge characteristics matter more than most dosing charts account for. Higher feed solids concentration, changes in digestion (anaerobic vs. aerobic), and even seasonal shifts in sludge age can all change the optimal dose. A dose that was correct for your sludge in March isn't guaranteed to be correct in July, run a quick jar test whenever cake quality drifts rather than assuming the equipment has a mechanical problem.
Track polymer dose, feed solids, and resulting cake solids together, not in isolation. That combined dataset is what actually lets you spot a real optimal-dose drift versus a one-off feed sludge anomaly.
Mixing energy at the point of polymer injection is frequently the hidden variable behind inconsistent dewatering results. Too little mixing means polymer never fully disperses through the sludge, effectively underdosing even when the metering pump is calibrated correctly. Too much mixing shears the flocs apart after they've formed, which looks identical to underdosing on the belt even though the dose itself was correct. If dose adjustments aren't fixing a cake quality problem, check injection point mixing before assuming the polymer chemistry is wrong.
Polymer selection (cationic charge density and molecular weight) needs to match your specific sludge type, and a product that performs well on anaerobically digested sludge may underperform on aerobically digested or waste activated sludge from the same plant. Most polymer vendors will run a jar test series across several product options when cake quality plateaus, it's worth requesting this rather than assuming your current product is still the best fit as feed sludge characteristics drift over time.
Temperature affects both polymer performance and sludge viscosity. Cold conditioning water or cold ambient temperatures can slow polymer hydration (especially for dry polymer systems, which need adequate mixing time to fully activate) and reduce dewatering performance independent of dose. If cake quality consistently drops in winter months, check makeup water and polymer solution temperature before assuming feed sludge itself has changed.
Finally, track the cost side alongside the process side. Because polymer is one of the largest chemical costs at most plants, a small dose reduction that maintains acceptable cake solids can produce meaningful annual savings. Run periodic dose-reduction trials in small increments during stable operating periods (not during a cake quality problem) to find the true minimum effective dose rather than defaulting to a comfortable, higher-than-necessary setpoint.
A useful benchmarking practice: track polymer cost per dry ton of cake produced, not just polymer dose per gallon of sludge fed. This normalizes for changes in feed solids concentration and makes it possible to compare dewatering economics across different periods or even different equipment fairly.
When troubleshooting a sudden cake solids drop, check feed sludge characteristics (solids concentration, VS content, temperature) before assuming the polymer or equipment is at fault; a digester upset or thickening process change upstream often shows up first as a dewatering performance problem several days later.
Don't stop at the article.
The industry's most useful newsletter, straight from the plant floor.
One email. No fluff. New lessons, equipment breakdowns, and process control notes, delivered when there's something worth reading.